● Railway sector

Composites for rolling stock, compliant with EN 45545-2

We compression-mould interior and exterior parts for railway manufacturers and integrators: from long series in flame-retardant SMC to lightweight carbon fibre components. It is our reference sector, where our technical development is greatest.

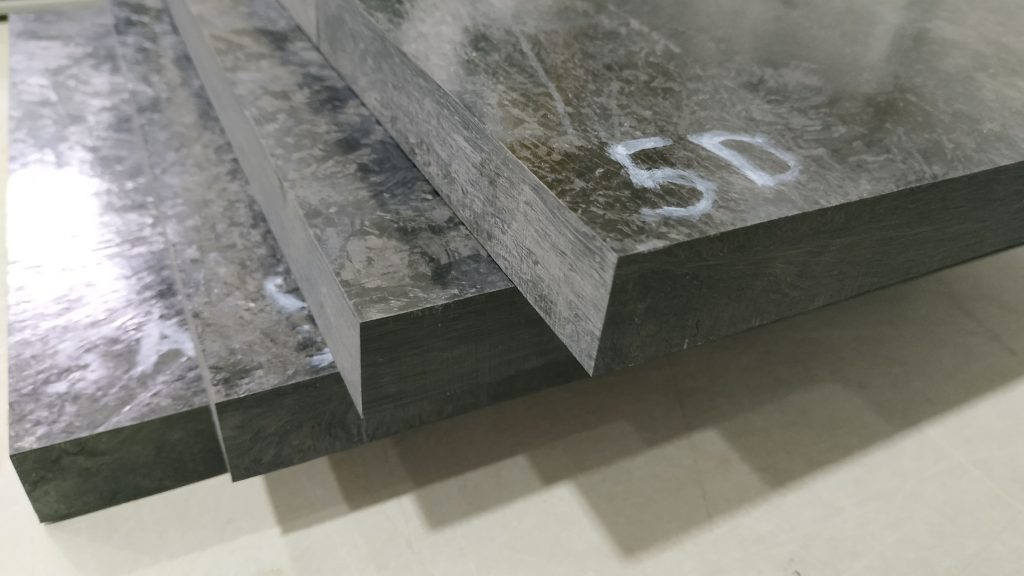
Railway part moulded in CSMC
HL3
highest EN 45545-2 level in our flame-retardant grades
R1 · R6 · R7
plus R2, R3, R17: classified requirements
3 materials
flame-retardant SMC, phenolic SMC and CSMC
1,250 t
largest press, 3,500 × 1,800 mm platen
3D explorer · Rail

Take a railcar apart and see which material goes into each part

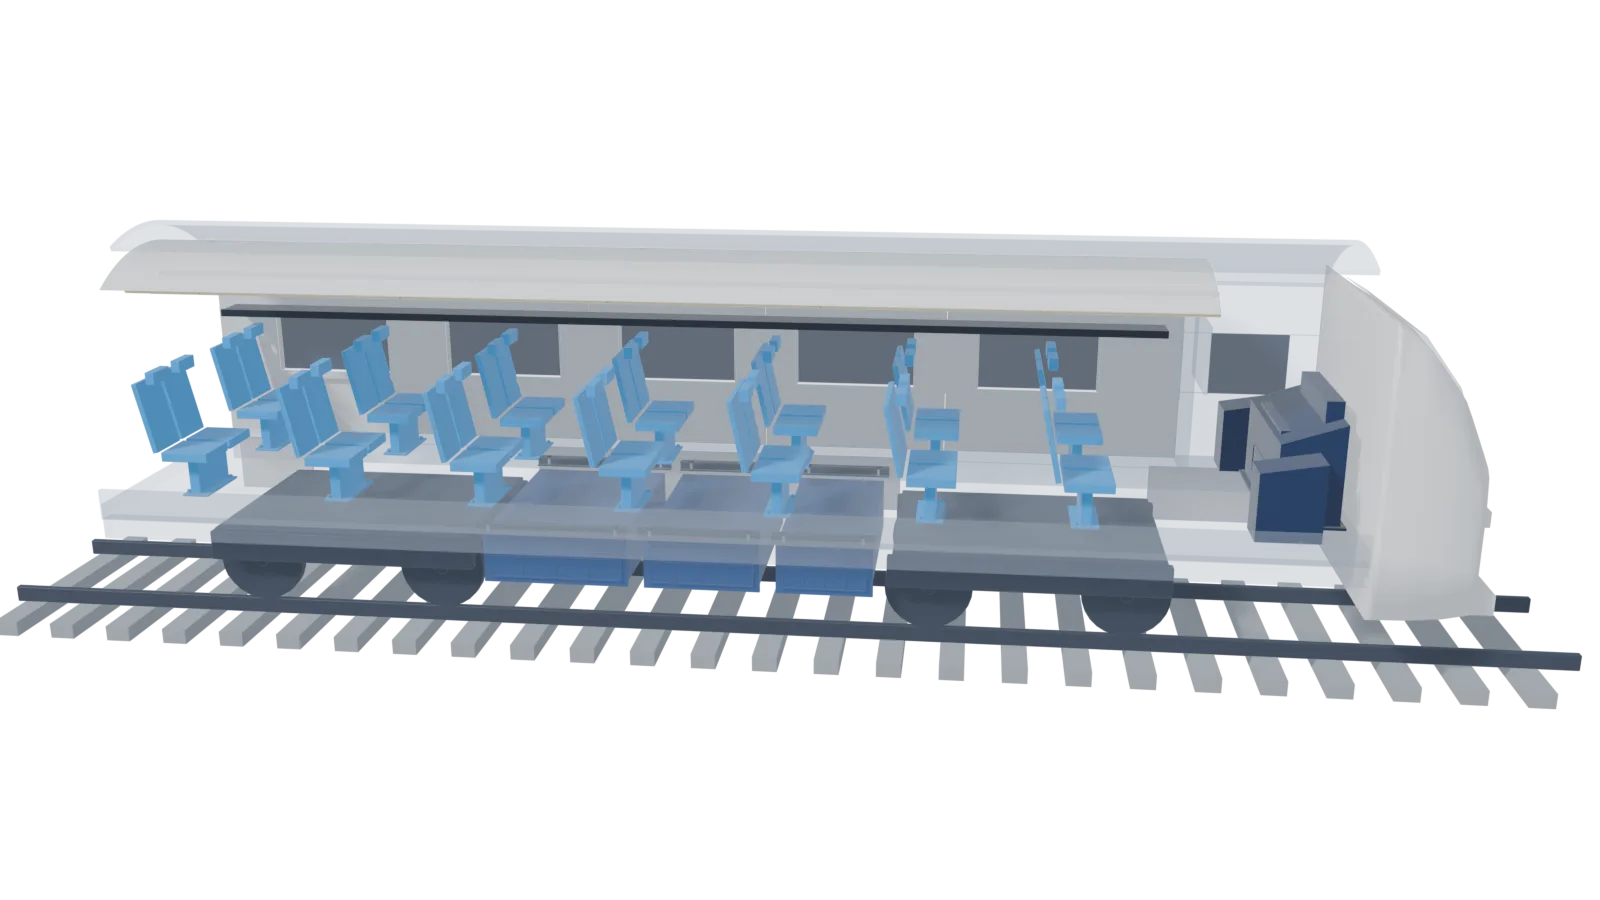
Generic passenger coach in cutaway, with the carbody in translucent grey. Click a part to zoom in and see its engineering sheet: process, fixing, lightweighting, advantages and series.

Render of a generic passenger coach in cutaway, with linings, ceiling, seats, driver desk, brackets, enclosures and front end

Drag to rotate · scroll or pinch to zoom · click a part to zoom in

01

Interior side panels

Location
Saloon walls, with 3D window frame.
Recommended material
Rail SMC HL3 · Structural Phenolic SMC 55% GF
Requirement / key data
EN 45545-2 · R1 up to HL3 (Rail SMC HL3). Alternative Structural Phenolic SMC: HL3, requirement depending on application.
1Part detail and process
Panel with 3D window frame, reveal and sill in a single pressing, rib grid on the back face and bosses with hidden inserts. Typical thickness of 2.5 to 6 mm for moulded parts. 5-axis waterjet trimming (0°–64°) and in-house CNC machining. Finish: technical visible face in the material colour.
2Assembly and fixing to the structure
  • M5–M12 threaded metal inserts, moulded in or installed cold or hot into reinforced bosses.
  • Perimeter overlap flanges to fit the adjacent parts.
3Lightweighting: ribbed monolithic or sandwich
Proposed solution: ribbed monolithic. Thin wall with 3D ribs, bosses and inserts where the loads arrive — right for compact parts or point loads. For large spans, a sandwich panel is assessed.
4Advantages over the traditional alternative
Compared with flat panels assembled with profiles — Rail SMC HL3: classified EN 45545-2 R1, R2, R3, R6, R7 and R17 up to HL3 by an ENAC-accredited laboratory; fewer parts and joints than an assembled solution.
5Series and manufacturing capacity
Typical series (indicative): 50 to 500 pcs/year, typical of rail, aerospace or space programmes. Press: P30 or P7 (6,000 kN, 1,850 × 1,400 and 1,600 × 1,400 mm platens). In-house fleet of 7 presses from 150 to 1,250 t, with a largest platen of 3,500 × 1,800 mm. The steel mould is amortised over the series: the higher the volume, the lower the tooling cost per part; for short runs we compare with other solutions.
Request a study of this part →
02

Curved modular ceiling with HVAC

Location
Saloon ceiling with air channels and diffusers.
Recommended material
Rail SMC HL3 · Structural Phenolic SMC 55% GF
Requirement / key data
EN 45545-2 · R1 up to HL3 (Rail SMC HL3). Alternative Structural Phenolic SMC: HL3, requirement depending on application.
1Part detail and process
Large curved sandwich module (layers visible at the cut), with integrated HVAC channel and louvred diffusers. Typical thickness of 2.5 to 6 mm for moulded parts. 5-axis waterjet trimming (0°–64°) and in-house CNC machining. Finish: technical visible face in the material colour.
2Assembly and fixing to the structure
  • M5–M12 threaded metal inserts, moulded in or installed cold or hot into reinforced bosses.
  • Perimeter overlap flanges to fit the adjacent parts.
3Lightweighting: ribbed monolithic or sandwich
Proposed solution: sandwich panel. Moulded skins with a lightweight self-extinguishing core, selected for the fire requirement, multiply flexural stiffness over large spans compared with a monolithic panel of the same weight; the actual weight saving is quantified in each part study. Compact parts are solved as ribbed monolithic.
4Advantages over the traditional alternative
Compared with flat panels assembled with profiles — Rail SMC HL3: classified EN 45545-2 R1, R2, R3, R6, R7 and R17 up to HL3 by an ENAC-accredited laboratory; fewer parts and joints than an assembled solution.
5Series and manufacturing capacity
Typical series (indicative): 50 to 500 pcs/year, typical of rail, aerospace or space programmes. Press: P10 (1,250 t, 3,500 × 1,800 mm platen) or P8 (10,000 kN, 2,800 × 1,800 mm). In-house fleet of 7 presses from 150 to 1,250 t, with a largest platen of 3,500 × 1,800 mm. The steel mould is amortised over the series: the higher the volume, the lower the tooling cost per part; for short runs we compare with other solutions.
Request a study of this part →
03

Load-bearing seat shells

Location
Backrest, seat and pedestal of each seat.
Recommended material
Rail SMC HL3
Requirement / key data
EN 45545-2 · R6 up to HL3 (Rail SMC HL3).
1Part detail and process
Vandal-resistant shell with rear rib grid, headrest and bosses with metal inserts for fixing to the pedestal. Typical thickness of 2.5 to 6 mm for moulded parts. 5-axis waterjet trimming (0°–64°) and in-house CNC machining. Finish: technical visible face in the material colour.
2Assembly and fixing to the structure
  • M5–M12 threaded metal inserts, moulded in or installed cold or hot into reinforced bosses.
  • Metal torque-limiting bushings in through holes, so tightening does not cause composite creep under vibration.
3Lightweighting: ribbed monolithic or sandwich
Proposed solution: ribbed monolithic. Thin wall with 3D ribs, bosses and inserts where the loads arrive — right for compact parts or point loads. For large spans, a sandwich panel is assessed.
4Advantages over the traditional alternative
Compared with cut, welded and painted steel sheet — Rail SMC HL3: classified EN 45545-2 R1, R2, R3, R6, R7 and R17 up to HL3 by an ENAC-accredited laboratory; fewer parts and joints than an assembled solution.
5Series and manufacturing capacity
Typical series (indicative): 50 to 500 pcs/year, typical of rail, aerospace or space programmes. Press: P22 or P20 (4,000 and 2,500 kN, 1,000 × 1,000 and 800 × 800 mm platens). In-house fleet of 7 presses from 150 to 1,250 t, with a largest platen of 3,500 × 1,800 mm. The steel mould is amortised over the series: the higher the volume, the lower the tooling cost per part; for short runs we compare with other solutions.
Request a study of this part →
04

Driver’s desk

Location
Driving console with side modules.
Recommended material
SMC + PIMC in-mould painting, Class A
Requirement / key data
EN 45545-2 depending on its position in the cab: defined for each project.
1Part detail and process
One-piece ergonomic desk with control recess, instrument hood, ventilation grille and fixing flange with inserts. Typical thickness of 2.5 to 6 mm for moulded parts. 5-axis waterjet trimming (0°–64°) and in-house CNC machining. Finish: PIMC in-mould painting, Class A.
2Assembly and fixing to the structure
  • M5–M12 threaded metal inserts, moulded in or installed cold or hot into reinforced bosses.
  • Perimeter overlap flanges to fit the adjacent parts.
3Lightweighting: ribbed monolithic or sandwich
Proposed solution: ribbed monolithic. Thin wall with 3D ribs, bosses and inserts where the loads arrive — right for compact parts or point loads. For large spans, a sandwich panel is assessed.
4Advantages over the traditional alternative
Compared with cut, welded and painted steel sheet — SMC with PIMC in-mould painting: Class A finish straight from the press, with no paint booth afterwards and no corrosion.
5Series and manufacturing capacity
Typical series (indicative): 50 to 500 pcs/year, typical of rail, aerospace or space programmes. Press: P30 or P7 (6,000 kN, 1,850 × 1,400 and 1,600 × 1,400 mm platens). In-house fleet of 7 presses from 150 to 1,250 t, with a largest platen of 3,500 × 1,800 mm. The steel mould is amortised over the series: the higher the volume, the lower the tooling cost per part; for short runs we compare with other solutions.
Request a study of this part →
05

Equipment beams and brackets

Location
Underfloor frames and luggage rack brackets.
Recommended material
CSMC Carbon 57%
Requirement / key data
Secondary structure. The CSMC datasheet includes no EN 45545-2 classification: in areas with a fire requirement it is validated in the study.
1Part detail and process
I-beams and brackets with web and flanges moulded in one go, with compression bushings and galvanic insulation washers at each support. Typical thickness of 2.5 to 6 mm for moulded parts. 5-axis waterjet trimming (0°–64°) and in-house CNC machining. Finish: technical visible face with controlled roughness in bonding areas.
2Assembly and fixing to the structure
  • Metal torque-limiting bushings in through holes, so tightening does not cause composite creep under vibration.
  • Galvanic couple insulation (insulating washers and gaskets) where the carbon part is fixed onto aluminium.
  • M5–M12 threaded metal inserts, moulded in or installed cold or hot into reinforced bosses.
3Lightweighting: ribbed monolithic or sandwich
Proposed solution: ribbed monolithic. Thin wall with 3D ribs, bosses and inserts where the loads arrive — right for compact parts or point loads. For large spans, a sandwich panel is assessed.
4Advantages over the traditional alternative
Compared with machined or cast aluminium — CSMC Carbon 57%: 1.51 g/cm³ vs 2.70 for aluminium (−44% at equal volume), tensile 370 MPa, modulus 41.5 GPa and +113% specific strength (245 vs 115 MPa·cm³/g).
5Series and manufacturing capacity
Typical series (indicative): 50 to 500 pcs/year, typical of rail, aerospace or space programmes. Press: P22 or P20 (4,000 and 2,500 kN, 1,000 × 1,000 and 800 × 800 mm platens). In-house fleet of 7 presses from 150 to 1,250 t, with a largest platen of 3,500 × 1,800 mm. The steel mould is amortised over the series: the higher the volume, the lower the tooling cost per part; for short runs we compare with other solutions.
Request a study of this part →
06

Underframe electrical enclosures

Location
Equipment enclosures and internal insulating plate.
Recommended material
Electrical SMC V-0 / CTI 600
Requirement / key data
UL 94 V-0 (3 mm) · glow wire 960 °C · CTI 600 · 16 kV/mm. EN 45545-2 depending on location: confirmed for each project.
1Part detail and process
Enclosure with ribbed lid, labyrinth sealing lip, ventilation grille and inserts at the lid corners. Typical thickness of 2.5 to 6 mm for moulded parts. 5-axis waterjet trimming (0°–64°) and in-house CNC machining. Finish: technical visible face in the material colour.
2Assembly and fixing to the structure
  • M5–M12 threaded metal inserts, moulded in or installed cold or hot into reinforced bosses.
  • Perimeter lip or channel for a sealing elastomer gasket.
  • Hinge and lock seats moulded with their inserts, with no welded reinforcements.
3Lightweighting: ribbed monolithic or sandwich
Proposed solution: ribbed monolithic. Thin wall with 3D ribs, bosses and inserts where the loads arrive — right for compact parts or point loads. For large spans, a sandwich panel is assessed.
4Advantages over the traditional alternative
Compared with cut, welded and painted steel sheet — Electrical SMC V-0 / CTI 600: 16 kV/mm, CTI 600, glow wire 960 °C, HDT > 250 °C, dielectric constant 4 and UL 94 V-0 at 3 mm. Corrosion-free, weld-free and inherently insulating.
5Series and manufacturing capacity
Typical series (indicative): 50 to 500 pcs/year, typical of rail, aerospace or space programmes. Press: P30 or P7 (6,000 kN, 1,850 × 1,400 and 1,600 × 1,400 mm platens). In-house fleet of 7 presses from 150 to 1,250 t, with a largest platen of 3,500 × 1,800 mm. The steel mould is amortised over the series: the higher the volume, the lower the tooling cost per part; for short runs we compare with other solutions.
Request a study of this part →
07

Aerodynamic front end and skirts

Location
Front fairing and large-format skirts.
Recommended material
Structural Phenolic SMC 55% GF
Requirement / key data
Structural Phenolic SMC: UL 94 V-0 @ 1.2 mm and LOI > 100%. Where the specification requires R7 (exterior), Rail SMC HL3 covers it.
1Part detail and process
Large front end with louvred air intake and headlight seats, and skirts with rear ribs and inserts; moulded on the 1,250 t press. Typical thickness of 2.5 to 6 mm for moulded parts. 5-axis waterjet trimming (0°–64°) and in-house CNC machining. Finish: technical visible face in the material colour.
2Assembly and fixing to the structure
  • M5–M12 threaded metal inserts, moulded in or installed cold or hot into reinforced bosses.
  • Perimeter overlap flanges to fit the adjacent parts.
  • Metal torque-limiting bushings in through holes, so tightening does not cause composite creep under vibration.
3Lightweighting: ribbed monolithic or sandwich
Proposed solution: ribbed monolithic. Thin wall with 3D ribs, bosses and inserts where the loads arrive — right for compact parts or point loads. For large spans, a sandwich panel is assessed.
4Advantages over the traditional alternative
Compared with flat panels assembled with profiles — Structural Phenolic SMC 55% GF: 1.84 g/cm³, flexural 350 MPa, Charpy 120 kJ/m², UL 94 V-0 at 1.2 mm, LOI > 100% and 0.00% moulding shrinkage (indicative datasheet values). A single 3D part with no bolted joints.
5Series and manufacturing capacity
Typical series (indicative): 50 to 500 pcs/year, typical of rail, aerospace or space programmes. Press: P10 (1,250 t, 3,500 × 1,800 mm platen) or P8 (10,000 kN, 2,800 × 1,800 mm). In-house fleet of 7 presses from 150 to 1,250 t, with a largest platen of 3,500 × 1,800 mm. The steel mould is amortised over the series: the higher the volume, the lower the tooling cost per part; for short runs we compare with other solutions.
Request a study of this part →

Generic, illustrative model: it does not represent any real vehicle. Indicative recommendations: the final choice depends on the R requirement, HL level and thickness of each project. EN 45545-2 classifications apply to the tested material and are not a type approval of the part.

Three materials, one plant

The right material for every part of the train.

01

Flame-retardant polyester SMC: for volume

Grades with aluminium trihydroxide, classified to EN 45545-2 for R1, R2, R3, R6, R7 and R17 up to HL3 by an ENAC-accredited laboratory. The most competitive option for long series of linings, covers and housings.

02

Phenolic SMC: chemistry-based fire behaviour

For parts where the resin’s inherent fire behaviour comes first; HL3 certified configuration. See phenolic SMC →

03

CSMC: when weight is key

Compression-moulded carbon fibre with 113% higher specific strength than 6061-T6 aluminium, for lightweight structural components. See CSMC →

EN 45545-2

How a material is classified under EN 45545-2

The standard classifies each material against a requirement (R), according to the part’s location and function (for example R1 for interior linings or R6 for seats), and a hazard level (HL1–HL3), which depends on the vehicle’s operation and design category.

The tests measure flame spread (ISO 5658-2), heat release (ISO 5660-1), smoke density (ISO 5659-2) and gas toxicity (Annex C). For each part we confirm with the customer the requirement and level their specification calls for, and provide the material documentation.

Technical data

EN 45545-2 materials we work with

Material Requirements Level Document
Rail SMC HL3 (flame-retardant polyester, 1.97 g/cm³) R1, R2, R3, R6, R7, R17 HL1, HL2 and HL3 Classification report, ENAC-accredited laboratory (2015)
Rail SMC HL2 (flame-retardant polyester) R1, R2, R3, R6, R7, R17 HL1 and HL2 ENAC classification report (2014); tests repeated in 2021
Phenolic SMC Depending on application HL3 We confirm the classification for your part

Classifications refer to the tested material (without substrate and valid for any colour, per EN 45545-2:2013) and are not a type approval of the part: compliance depends on thickness, location and the applicable requirement in each project. Values from the material manufacturer’s datasheet and classification reports from an ENAC-accredited laboratory. Documentation available on request.

Applications

Parts we make for the sector

  • Interior linings: walls, ceilings and partitions.
  • Covers, housings and technical caps.
  • Seat components.
  • Exterior vehicle parts.
  • Lightweight structural components in CSMC.
Fire-retardant phenolic SMC material
Application cases

Types of railway project we solve.

Illustrative examples of the kind of technical and commercial challenge we take on — they don't correspond to a specific identifiable client.

Interior lining: material change to save weight

Challenge: a rolling stock manufacturer needed to reduce the weight of an aluminium interior panel without losing stiffness or compromising the fire behaviour required for interiors (EN 45545-2, requirement R1).

Solution: panel redesigned in phenolic SMC, adjusting thicknesses and ribs to match the stiffness of aluminium at lower weight.

Result: a lighter part, keeping the required fire classification.

Structural component: long series without delays

Challenge: an integrator with several of its own moulds could not get its supplier to take on long series at the rate the programme needed.

Solution: production redistributed across our 7 presses according to each mould’s tonnage and cycle, freeing capacity for larger batches.

Result: long series covered steadily, with predictable lead times.

Lightweight component: from aluminium to CSMC

Challenge: an aluminium structural component penalised vehicle weight and assembly cost.

Solution: replaced with CSMC, redesigning thicknesses to exploit its higher specific strength.

Result: a lighter component, meeting the programme’s structural requirements.

Industrial capacity

From mould to finished part, in a single plant.

7
compression presses, from 150 to 1,250 t
3.500 × 1.800
mm platen on our largest press
24 Tn
moulds up to 24 tonnes, with a dedicated mould store
CNC + 5 ejes
4 CNC centres and 2 in-house waterjet cutting machines
PIMC
in-mould painting for a Class A finish
ISO 9001 · 14001
quality and environment, unit traceability batch–press–part
Frequently asked questions

Common questions from railway manufacturers

Which hazard level do I need?

It is set by EN 45545-1 from the vehicle’s operation and design category, and is usually fixed in the train manufacturer’s specification. Tell us the level and requirement and we will propose the material.

Phenolic or flame-retardant polyester SMC?

Flame-retardant polyester reaches its classification with fillers such as aluminium trihydroxide and is the most competitive option for volume; phenolic owes its fire behaviour to the resin itself. We choose based on requirement, weight, volume and cost.

Can you support us from the design stage?

Yes: in-house engineering with CAD/CAM (SolidWorks, CamWorks) and 3D printing for prototypes, working with the customer’s engineering team from the concept phase.

What volumes can you handle?

Both short runs and long-term programmes: with 7 presses from 150 to 1,250 t we allocate load by mould and cycle. Share the programme forecast and we will plan it.

Running a railway programme?

Tell us about the part, the EN 45545-2 requirement and level, and the programme volume: we will propose the material and confirm initial feasibility within 24 working hours.